- Filtration accuracy
- 5μm - 500μm
- Temperature range
- 0°C - 250°C
- Flow rate
- 2 - 150 m³/h
- Operating pressure
- 0.4 MPa - 0.6 MPa

Enclosed Pressure Filtration for Fine Particles, High-purity Liquids and Automated Filter-cake Discharge in Chemical, Pharmaceutical and Industrial Processes.
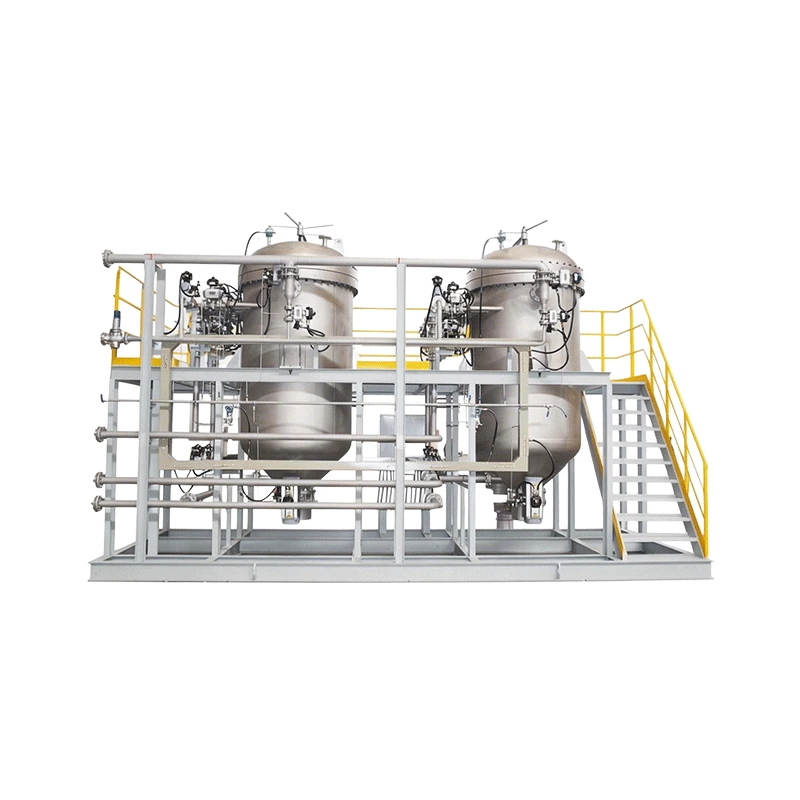
UNITE industrial candle filter systems are enclosed pressure filtration solutions designed for high-efficiency solid-liquid separation. The system uses vertical tubular candle elements to retain fine solid particles while allowing clarified liquid to pass through the filter media.
With automatic backwashing, gas blowback, filter-cake washing, drying and discharge options, the U-CF-S series supports repeatable filtration cycles with minimal manual intervention. The fully enclosed design helps reduce product exposure, leakage risk and contamination, making it suitable for hazardous, corrosive, high-temperature and high-value process materials.
UNITE candle filter systems are widely used in fine chemicals, pharmaceuticals, petrochemicals, battery materials, food processing and other industries that require reliable filtration performance, high product purity and customized process control.
With filtration precision from 0.2 to 100 microns, flexible filter element and housing materials, PLC-based control and skid-mounted integration, UNITE provides complete candle filter solutions based on your slurry properties, flow rate, pressure, temperature and cake-discharge requirements.
Get Custom Quote Within 24h or Download Filter Catalog
Send your slurry data and filtration requirements to our engineers.
Fully Enclosed Filtration
The sealed filter housing helps reduce product exposure, leakage risk and contamination during filtration of hazardous, volatile or high-value materials.
Efficient Filter-Cake Formation
Solid particles are retained on the outer surface of the candle elements to form a uniform filter cake. The cake can be washed, dried or discharged according to the process requirements.
Automatic Cake Removal
Backwashing, gas blowback or other configured cleaning methods remove the filter cake without opening the vessel, reducing manual intervention and process downtime.
Flexible Process Skid Design
UNITE can integrate the filter housing, valves, instruments, piping and PLC control system into a complete skid-mounted filtration package.
Materials for Demanding Processes
Filter elements and housing materials can be selected according to process chemistry, temperature, pressure, corrosion resistance and product purity requirements.

The slurry enters the enclosed filter housing under controlled pressure. The liquid passes through the filter media, while solid particles are retained on the outer surface of the vertical candle elements.
As filtration continues, the retained solids form a filter cake. The clarified liquid flows through the candle elements and exits through the filtrate outlet. Differential pressure monitoring indicates when the cake has reached the required thickness.
Depending on the process, the filter cake can be washed, dried, backwashed or removed by gas blowback. The solids are then discharged through the bottom outlet, while the closed vessel remains sealed during the filtration cycle.

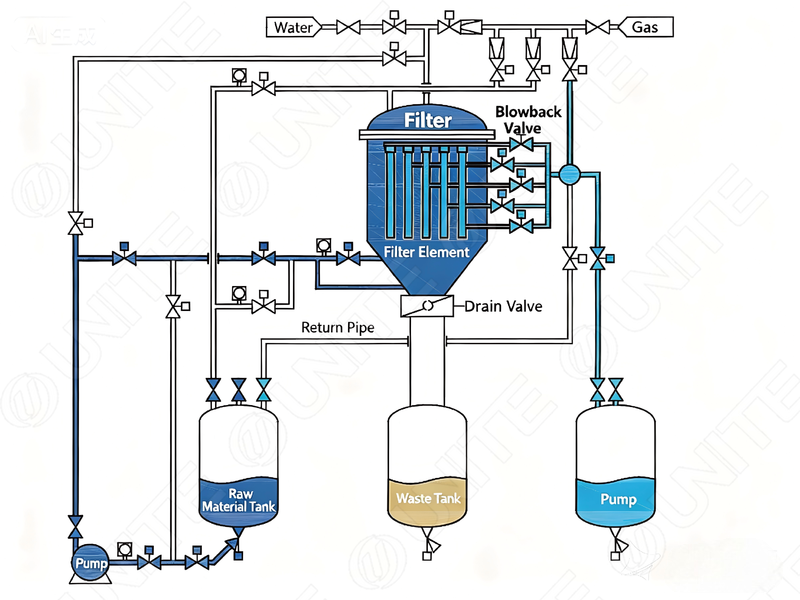
When the solid-liquid mixture passes through the filter, solid particles are retained on the outer surface of the filter element and accumulate to form a filter cake. This leads to a gradual increase in the pressure difference between the inlet and outlet of the filter. When the pressure difference reaches a preset value, it indicates that the filter cake has attained a certain volume or thickness. This condition is simultaneously detected and controlled by a thickness sensor.
At this stage, the positive pressure process is initiated to continue pressing the liquid phase within the filtration tank. Once all the liquid in the tank has been pressed out and the residual liquid has been handled, the cake removal process commences.
The backflush valve is opened, while the inlet and outlet valves are closed, and the slag discharge valve is opened. Due to the backflush air, the filter cake expands instantaneously and is discharged through the bottom slag discharge valve into a solid-phase conveying or collection device.
The following specifications are reference ranges. Final design parameters depend on slurry properties, filtration duty, material compatibility, required cake handling and applicable project standards.
| Parameter Item | Details |
|---|---|
| Equipment Model | U-CF-S, S1, S2, SS |
| Filtration Precision | 0.2 - 100 microns, depending on the filter element and functional design |
| Standard Design Pressure Rating | 0.6MPA/1.0MPA/1.6MPA/2.0MPA; higher pressures can be customized |
| Filter Element | PVDF, PTFE, PPS, PP, titanium materials, etc. |
| Maximum Design Temperature | 0 - 300°C |
| Flow Rate Range | 10 - 300M³/H |
| Filtration Area | 0.9m² - 150m²; larger specifications can be customized |
| Cylinder Diameter | Φ250 - Φ2500 |
| Back - blow Pressure Difference | 0.2MPA - 0.3MPA |
| Control System | PLC |
| Inlet and Outlet Sizes | 2" - 24" |
| Housing Material | 304/316L/CS/duplex steel/titanium; special materials can be customized |
| Internal Anti - corrosion Coating | Rubberized (suitable for carbon steel or special anti - corrosion requirements) |
| Housing Sealing Material | NBR nitrile rubber (standard)/VITON (FKM) fluororubber/metal graphite gasket |
| Drain Valve | Soft - sealed or hard - sealed butterfly valve |
| Optional Automation Control | Pressure/pressure - sensing transmitter, liquid level switch, filter cake thickness detector, flow meter, temperature meter, oxygen analyzer, etc. |
A candle filter is suitable when a process requires enclosed, fine solid-liquid separation with controlled filter-cake formation and limited manual intervention.
It is commonly considered when you need:
- High-clarity filtrate from a slurry or suspension
- Fine particle retention and repeatable filtration cycles
- Enclosed processing for hazardous, volatile or high-value materials
- Automated backwashing, cake washing, drying or discharge
- Low product loss and reduced operator exposure
- Filtration of corrosive or high-temperature process fluids
The correct candle filter design depends on slurry concentration, particle size, viscosity, temperature, pressure, required filtrate quality, cake properties and the desired cake discharge method.
| Equipment | Best suited for | Main consideration |
| Candle Filter | Fine filtration, enclosed processing and automated cake handling | Filter element design, cake formation and discharge method |
| Pressure Leaf Filter | Batch clarification and filter-aid filtration | Filtration area, cake handling and maintenance method |
| Filter Press | High-solids batch dewatering | Labour, cycle time and cake discharge |
| Cartridge Filter | Low-solids polishing filtration | Consumable replacement and operating cost |
Talk to Our Engineers to Get a Free, Customized Filtration Solution.
Send your slurry data and filtration requirements to receive a suitable candle filter configuration from UNITE engineers.
A Candle Filter is a pressure-driven filtration system that uses vertical cylindrical filter elements (candle-like structures) to separate solids from liquids. It is commonly used for high-efficiency solid-liquid separation and cake filtration.
The slurry is fed into a closed pressure vessel, where liquid passes through the porous candle elements while solids form a filter cake on the surface. The cake is later discharged by backwashing, vibration, or gas blowback.
Key advantages include high filtration efficiency, ability to handle high solids concentration, closed system operation (no leakage or contamination), low moisture cake discharge, and suitability for automated operation.
Candle filters are widely used in chemical processing, pharmaceuticals, petrochemicals, fine chemicals, metallurgy, and lithium battery materials production, especially for fine particle separation and high-purity requirements.
A candle filter uses vertical tubular elements and is better for fine filtration and automation, while a pressure leaf filter uses flat leaves and is more suitable for larger filtration areas and coarser slurries.
Candle filters can be configured for chemical, pharmaceutical, petrochemical, food, battery material and other process liquids. Filter element and housing materials are selected according to fluid chemistry, temperature, pressure and product purity requirements.
Yes. A candle filter system can be equipped with PLC control, differential pressure monitoring, backwashing, gas blowback, cake thickness detection, liquid-level control and automatic cake discharge according to the process requirements.
UNITE engineers typically need the slurry composition, solid concentration, particle size, viscosity, flow rate, operating pressure, operating temperature, required filtrate quality, cake properties and desired cleaning or discharge method.


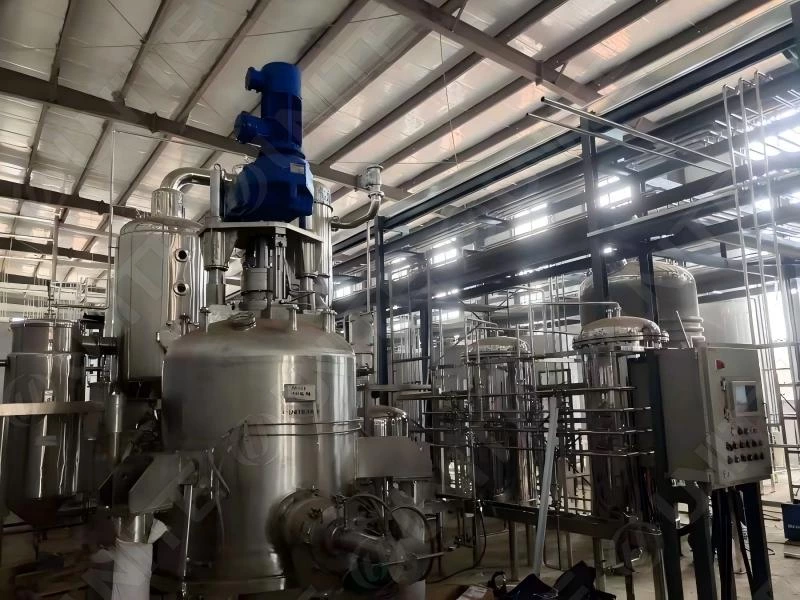
For high-value, oxidation-sensitive fine chemical materials containing volatile organic compounds (VOCs), UNITE supplied BASF with a modular integrated system comprising a candle filter and a three-in-one filter dryer, also known as an Agitated Nutsche Filter Dryer (ANFD). The solution combines precision pre-clarification, solid-liquid separation, filter-cake washing, vacuum drying, and automatic discharge within an enclosed process. After commissioning, the project achieved a historic high in product purity, increased solvent recovery by 25%, and effectively eliminated odor leakage.

The filtration area of a single set of candle filter for this project reaches 115 square meters and above, with significant differences from small-specification equipment in terms of structural design, process design and detailed considerations.

Unite's full-automatic candle filter is applied to the solid-liquid separation of high-salt wastewater in the PPS new material project of Xinhech


We use cookies to collect information about how you use this site. We use this information to make the website work as well as possible and improve our services.more details