- Filtration accuracy
- 0.5μm - 200μm
- Temperature range
- -10°C - 200°C
- Flow rate
- 5 - 200 m³/h
- Operating pressure
- 0.6 MPa - 1.0 MPa

Agitated Nutsche Filter Dryer (ANFD) for Enclosed Solid-liquid Separation, Filter-cake Washing, Vacuum Drying, and Contained Discharge.
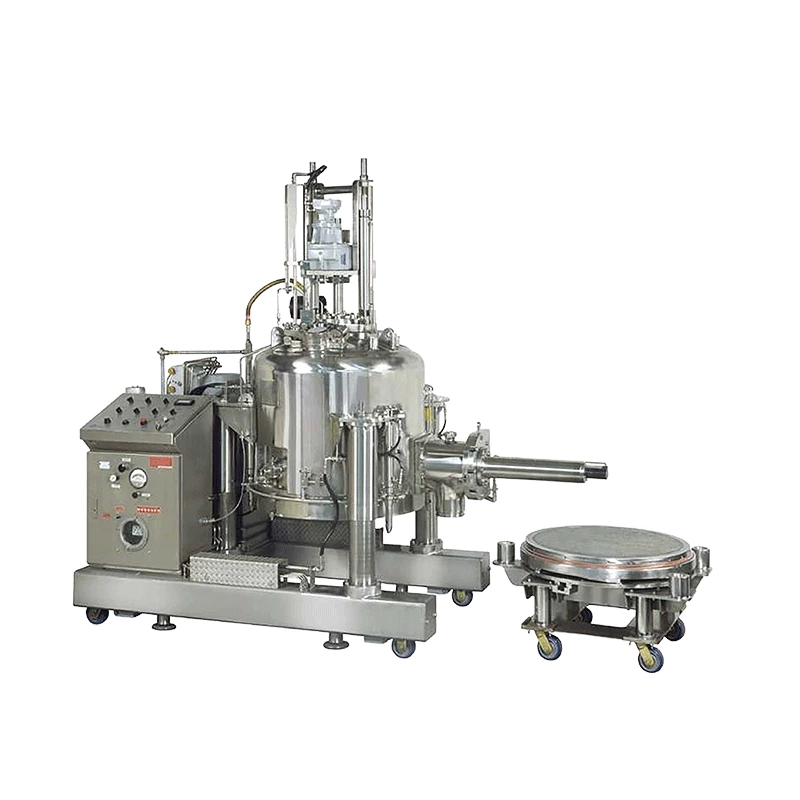
The Unite Agitated Nutsche Filter Dryer is a new-generation solid-liquid separation process equipment developed from advanced filtration technology. It integrates filtration, washing, and drying processes within a single fully enclosed vessel, maximizing equipment utilization and process efficiency.
The enclosed design prevents environmental contamination and material pollution, reduces material transfer losses, and minimizes solvent consumption. It is especially suitable for intermittent batch production processes requiring high cleanliness, safety, and efficient operation.
Designed for enclosed solid-liquid separation, cake washing, and drying in:
Suitable for applications requiring controlled washing, vacuum drying, low product transfer, and contained powder discharge.
Integrated Three-in-One Processing
Combines solid-liquid separation, filter-cake washing, and drying in one enclosed vessel.
Efficient Cake Management
The height-adjustable agitator levels, mixes, washes, dries, and discharges the filter cake according to process requirements.
Reliable Side Discharge
Available with manual or automatic side discharge valves and metal-to-metal or soft-seal configurations.
Improved Washing and Drying
Agitation supports cake washing and reslurry operations, while vacuum, hot-gas, jacket, or heated-agitator systems can be selected for drying.
Closed and Contained Operation
The enclosed design reduces product transfer, contamination risk, solvent loss, and operator exposure.
CIP and SIP Options
CIP and SIP systems are available for pharmaceutical, sterile, and high-purity processing applications.

An Agitated Nutsche Filter Dryer combines filtration, cake washing, drying, and solids discharge in one enclosed vessel.
Slurry Charging
The solid-liquid slurry enters the vessel and is distributed over the filter plate.
Pressure or Vacuum Filtration
Pressure or vacuum drives the liquid through the filter medium while solids form a filter cake.
Cake Washing or Reslurry
Washing liquid removes residual impurities and mother liquor. Agitation can resuspend the cake when deeper washing is required.
Vacuum or Hot-Gas Drying
The cake is dried using vacuum, heated surfaces, hot gas, inert gas, or a combination of these methods.
Contained Side Discharge
The agitator moves the dried product toward the side discharge valve for manual, automatic, or contained removal.
The final process configuration depends on the material properties, solvent, cake permeability, drying target, and containment requirements.


UNITE Agitated Nutsche Filter Dryers can be configured according to the process, product, and production requirements.
Final specifications are selected according to the material, batch size, solvent, process conditions, and applicable design standards.
| Model | Filtration Area (m2) | Shell Diameter (mm) | Work Pressure (Mpa) | Nominal Volume (m3) | Filter Cake Height (mm) |
|---|---|---|---|---|---|
| MFCD - 600 | 0.28 | 600 |
-0.1~03 (likely a typo,
should be a pressure range
like 0 - 0.3 etc., here kept as presented)
|
0.2 | 150 |
| MFCD - 800 | 0.5 | 800 | 0.5 | 180 | |
| MFCD - 1000 | 0.75 | 1000 | 0.75 | 250 | |
| MFCD - 1200 | 1.1 | 1200 | 1.3 | 250 | |
| MFCD - 1400 | 1.5 | 1400 | 1.8 | 300 | |
| MFCD - 1600 | 2 | 1600 | 2.8 | 350 | |
| MFCD - 1800 | 2.5 | 1800 | 4 | 350 | |
| MFCD - 2000 | 3.1 | 2000 | 4.8 | 400 | |
| MFCD - 2200 | 3.5 | 2200 | 5.5 | 400 | |
| MFCD - 2400 | 4.5 | 2400 | 6.5 | 450 | |
| MFCD - 2600 | 5.3 | 2600 | 8.7 | 450 | |
| MFCD - 2800 | 6 | 2800 | 12 | 450 | |
| MFCD - 3000 | 7 | 3000 | 13 | 500 | |
| MFCD - 3200 | 8 | 3200 | 14.5 | 500 | |
| MFCD - 3400 | 9 | 3400 | 15 | 500 | |
| MFCD - 3600 | 10 | 3600 | 20 | 500 | |
| MFCD - 3800 | 11.3 | 3800 | 23 | 500 |
An ANFD is suitable when filtration, cake washing, drying, and solids discharge are required in a controlled batch process.
Compared with separate filter and dryer equipment, an integrated ANFD can:
Separate equipment may be more suitable for continuous production, highly specialized drying, very high throughput, or products that are especially sensitive to agitation.
The correct choice should be based on filtration data, cake permeability, thermal and shear sensitivity, washing efficiency, drying behavior, and discharge performance. Laboratory or pilot testing may be recommended before final equipment sizing.
Please provide the following information so our engineers can recommend a suitable configuration:
Final equipment size and configuration are confirmed after reviewing the process data and application requirements.
Talk to Our Engineers to Get a Free, Customized Filtration Solution.
A Filter-Wash-Dry System is an integrated process equipment that performs solid-liquid separation, cake washing, and drying in a single closed vessel. It is widely used in industries requiring high purity and controlled processing conditions.
The system first filters slurry to form a solid cake, then washes the cake to remove impurities, and finally dries it using vacuum, inert gas, or thermal methods—all within the same unit without transferring materials.
Key advantages include fully enclosed operation, reduced contamination risk, lower material loss, improved product purity, reduced handling steps, and significant savings in labor and equipment footprint.
These systems are widely used in pharmaceuticals, fine chemicals, biotechnology, new energy materials (such as lithium battery production), and high-value chemical processing where purity and efficiency are critical.
Traditional processes require separate equipment for filtration, washing, and drying, increasing transfer loss and contamination risk. The integrated system combines all steps in one unit, improving efficiency and product consistency.


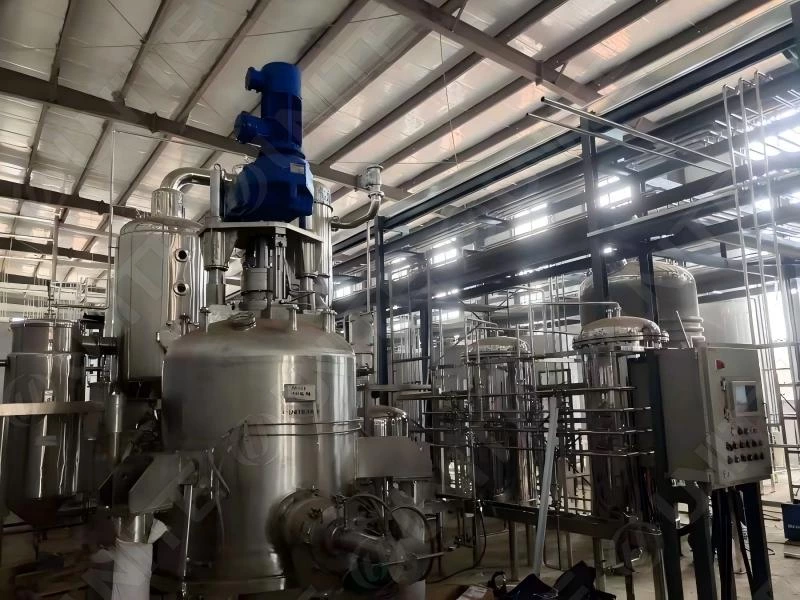
For high-value, oxidation-sensitive fine chemical materials containing volatile organic compounds (VOCs), UNITE supplied BASF with a modular integrated system comprising a candle filter and a three-in-one filter dryer, also known as an Agitated Nutsche Filter Dryer (ANFD). The solution combines precision pre-clarification, solid-liquid separation, filter-cake washing, vacuum drying, and automatic discharge within an enclosed process. After commissioning, the project achieved a historic high in product purity, increased solvent recovery by 25%, and effectively eliminated odor leakage.
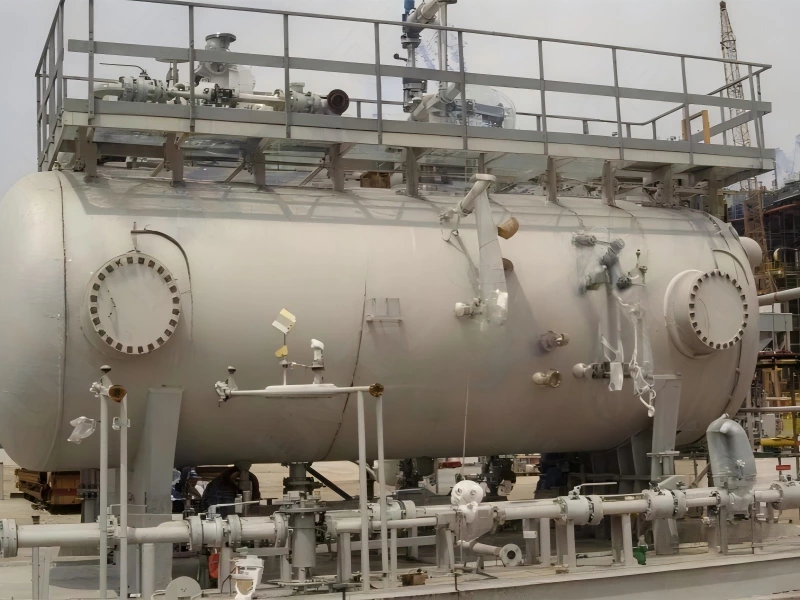
During the deep-processing and environmental-upgrade program at Kazakhstan’s Atyrau Refinery, UNITE supplied a modular three-phase separator for oily wastewater treatment and crude-oil pre-treatment. The system separates gas, liquid, and solid phases under high-flow, corrosive, and pressure-fluctuating conditions. It combines HIC-resistant or specially lined pressure-vessel construction, Hastelloy or super-stainless internal components, corrugated-plate mist elimination, cyclonic separation, coalescing elements, automated interface control, and all-weather insulation with electric heat tracing.

For Jiangxi Salt Chemical’s 55,000 t/y high-strength calcium sulfate project, UNITE supplied multiple large-scale automatic candle filters that integrate solid-liquid separation, displacement washing, pressure dewatering, back-pulse cake release, automatic discharge, and PLC-based process control. The project improved filter-cake washing, supported calcium sulfate quality above the stated industry benchmark, and reduced manual maintenance costs by approximately 60% compared with traditional filtration equipment.


We use cookies to collect information about how you use this site. We use this information to make the website work as well as possible and improve our services.more details